VBT-DB / DBT SERIES · COMPLETE ENGINEERING SOLUTION
Waste Oil to Base Oil Engineering Solution
A complete plant from feedstock testing and vacuum dehydration to lubricant-fraction recovery, product refining and grade-separated storage.
Designed for characterized used lubricating oil and waste mineral oil. The standard output is regenerated lubricant base oil. Capacity, technology route, viscosity cuts and guaranteed data are established from the real feedstock, product target and site conditions.
1–100 TPD
Capacity
80–90%*
Typical Product Yield
EPCM
Complete Project Service
PLC + SCADA
Automatic Control
CORE SEPARATION
05
Vacuum Distillation
Batch · Continuous · Thin Film
Feedstock-based design
Eight connected process units
Standard NCG energy recovery
Project-specific capacity
01
ENGINEERING SOLUTION
Project Overview
The VBT-DB / DBT plant conditions qualified used lubricating oil, applies one selected vacuum-distillation route, separates different base-oil fractions by fractionation and adds refining only when the product target requires it.
PROJECT PURPOSE
A buildable, operable and verifiable waste-oil-to-base-oil plant.
VBOLT turns the feedstock analysis, target viscosity grades, capacity, utilities and site conditions into process design, equipment configuration, automation, safety interlocks, manufacturing, commissioning, training and acceptance documents.
FEED
Used lubricating oil
Representative testing required
DISTILLATION
One of three routes
Batch, continuous or thin film
SEPARATION
Fractionation
Different base-oil fractions by boiling range
CAPACITY
Project-specific
10 T/D is one worked example
02
ENGINEERING SOLUTION
Design Basis & Feedstock Conditions
Plant capacity, technology route, vacuum duty, heating surface, product cuts and refining system are calculated only after representative used-oil data and operating conditions are defined.
Applicable Feedstocks
01 Waste engine oil
02Used lubricating oil
02Waste hydraulic oil
02Waste gear oil
02Waste transmission oil
02Tested waste mineral-oil blends
REQUIRED FEEDSTOCK TESTS
Test the oil before sizing the plant.
| Test Item | Engineering Use |
| Water | Dehydration load and heat demand |
| Solids / ash | Filtration, fouling and residue system |
| Density / viscosity | Pumping, heat transfer and target cuts |
| Sulfur / TAN | Refining route and product assessment |
| Distillation range | Base-oil recovery and cut points |
| Flash point | Safety and light-fraction assessment |
| Metals / additives | Fouling, colour and refining-media demand |
03
ENGINEERING SOLUTION
Target Product & Applications
The standard product is regenerated lubricant base oil. Its viscosity fractions and quality level depend on the feedstock, selected distillation route, fractionation cut points and optional refining system.
Base-oil quality is defined by complete laboratory data.
Release testing covers colour, density, kinematic viscosity at 40°C and 100°C, viscosity index, flash point, pour point, water, TAN, sulfur, ash and carbon residue.
STANDARD
Vacuum distillation, controlled fractionation and silica-gel or solvent refining can produce regenerated Group I-type base-oil fractions when supported by testing.
≥50 T/D UPGRADE
Large projects may select hydrotreating for higher product targets. Final product classification requires the complete process configuration and third-party test confirmation.
01
Colour
02
Viscosity 40°C
03
Viscosity 100°C
04
Viscosity Index
05
Flash Point
06
Pour Point
07
TAN / Sulfur
08
Ash / Carbon Residue
04
ENGINEERING SOLUTION
Complete Process Flow
The route is reception and testing, sedimentation and filtration, integrated vacuum dehydration and light-fraction removal, one selected distillation route, fractionation into different base-oil fractions, optional refining and grade-separated storage.
PROCESS UNIT 01
Waste Oil Reception & Testing
Receive, sample, test and classify each used-oil batch before processing.
INPUT
Used lubricating oil / waste mineral oil
OUTPUT
Accepted or isolated feedstock
CONTROL
Water, solids, density, viscosity, sulfur and distillation range
1 / 7
PROCESS UNIT 02
Sedimentation & Filtration
Remove free solids, sludge and suspended mechanical impurities before heating.
INPUT
Accepted waste oil
OUTPUT
Pre-treated oil and filter residue
CONTROL
Settling time, temperature, filter differential pressure and element condition
2 / 7
PROCESS UNIT 03
Vacuum Dehydration & Light Fraction Removal
Remove water first, then remove fuel-range and other low-boiling components in one integrated vacuum process unit.
INPUT
Pre-treated waste oil
OUTPUT
Conditioned oil, separated water and separately collected light fraction
CONTROL
Dehydration stage 55–180°C; light-removal stage 180–260°C; vacuum, condensation and separate collection
3 / 7
PROCESS UNIT 04
Selectable Distillation Route
One of Three Engineering Routes
Select batch twin-kettle, continuous tubular-furnace or thin-film vacuum distillation according to feedstock, capacity and operating mode.
INPUT
Conditioned used oil
OUTPUT
Base-oil vapour and separately discharged vacuum residue
CONTROL
Vacuum, temperature, feed rate, residence time, heating duty and residue discharge
4 / 7
PROCESS UNIT 05
Fractionation & Base Oil Fraction Separation
Separate base-oil vapour by boiling range before each fraction is condensed and collected.
INPUT
Base-oil vapour from the selected distillation route
OUTPUT
Separate light, medium and heavy base-oil fractions
CONTROL
Column temperature profile, reflux, cut points, condenser duty and product viscosity
5 / 7
PROCESS UNIT 06
Optional Refining
Select silica-gel adsorption, solvent extraction or hydrotreating for projects of 50 T/D or above according to the required product quality.
INPUT
Separated base-oil fractions
OUTPUT
Refined base oil and route-specific by-products
CONTROL
Adsorbent dosage, solvent ratio and recovery, or hydrogen pressure and catalyst conditions
6 / 7
PROCESS UNIT 07
Finished Base Oil Grade Storage
Store tested base-oil fractions in dedicated grade tanks with complete batch traceability.
INPUT
Qualified base-oil fractions
OUTPUT
Finished regenerated lubricant base oil by grade
CONTROL
Grade segregation, level, temperature, sampling, testing and release
7 / 7
05
ENGINEERING SOLUTION
Process Unit Description
Select any of the seven process units to see its purpose, inlet, outlet, equipment duty and key control conditions without opening a long page.
PROCESS UNIT 01
Waste Oil Reception & Testing
PURPOSE
Receive, sample, test and classify each used-oil batch before processing.
FEED
Used lubricating oil / waste mineral oil
OUTPUT
Accepted or isolated feedstock
KEY CONTROL
Water, solids, density, viscosity, flash point, sulfur, ash and distillation range
PROCESS UNIT 02
Sedimentation & Filtration
PURPOSE
Remove free solids, sludge and suspended mechanical impurities before heating.
FEED
Accepted used oil
OUTPUT
Pre-treated oil and filter residue
KEY CONTROL
Settling time, temperature, filter differential pressure and element condition
PROCESS UNIT 03
Vacuum Dehydration & Light Fraction Removal
PURPOSE
Remove water first, then remove fuel-range and other low-boiling components in one integrated vacuum process unit.
FEED
Pre-treated used oil
OUTPUT
Conditioned oil, separated water and separately collected light fraction
KEY CONTROL
Dehydration stage 55–180°C; light-removal stage 180–260°C; vacuum, condensation and separate collection
PROCESS UNIT 04
Selectable Distillation Route
PURPOSE
Select batch twin-kettle, continuous tubular-furnace or thin-film vacuum distillation according to feedstock, capacity and operating mode.
FEED
Conditioned used oil
OUTPUT
Base-oil vapour and separately discharged vacuum residue
KEY CONTROL
Vacuum, temperature, feed rate, residence time, heating duty and residue discharge
PROCESS UNIT 05
Fractionation & Base Oil Fraction Separation
PURPOSE
Separate base-oil vapour by boiling range before each fraction is condensed and collected.
FEED
Base-oil vapour from the selected distillation route
OUTPUT
Separate light, medium and heavy base-oil fractions
KEY CONTROL
Column temperature profile, reflux, cut points, condenser duty and product viscosity
PROCESS UNIT 06
Optional Refining
PURPOSE
Select silica-gel adsorption, solvent extraction or hydrotreating for projects of 50 T/D or above according to the required product quality.
FEED
Separated base-oil fractions
OUTPUT
Refined base oil and route-specific by-products
KEY CONTROL
Adsorbent dosage, solvent ratio and recovery, or hydrogen pressure and catalyst conditions
PROCESS UNIT 07
Finished Base Oil Grade Storage
PURPOSE
Store tested base-oil fractions in dedicated grade tanks with complete batch traceability.
FEED
Qualified base-oil fractions
OUTPUT
Finished regenerated lubricant base oil by grade
KEY CONTROL
Grade segregation, level, temperature, sampling, testing and release
OPTIONAL REFINING
Three quality routes, selected by project conditions.
Silica-gel adsorption and solvent extraction are optional refining systems. Hydrotreating is available only for projects of 50 T/D or above when higher product quality, hydrogen supply and investment conditions support it.
PRACTICAL POLISHING
Silica-Gel Adsorption
Adsorption removes selected polar compounds and improves colour, odour and storage stability. Spent silica gel is collected separately for compliant treatment.
SELECTIVE REFINING
Solvent Extraction
A project-selected extraction solvent separates aromatic and polar compounds. The engineering scope includes extraction, phase separation, solvent recovery and solvent purification.
LARGE-PROJECT UPGRADE
Hydrotreating
Hydrotreating is available only for projects of 50 T/D or above when feedstock testing, target quality, hydrogen supply and investment conditions support the route.
06
ENGINEERING SOLUTION
Material Balance
For every representative 10 tonnes of used oil processed, the page shows the quantity of regenerated base oil, water, light fraction, non-condensable gas and vacuum residue and where each stream goes.
INPUT BASIS
10 TON
Waste Oil Feed
One representative operating-day balance.
Regenerated base oil
8.0–8.5 t 80%–85%
Distillation vapour → fractionation → separate base-oil fractions → optional refining → grade storage
Separated water
<0.5 t <5%
Integrated vacuum unit → separate water collection → wastewater treatment
Light fraction
≈0.5 t≈5%
Integrated vacuum unit → separate light-fraction collection
Non-condensable gas
0.3–0.5 t3%–5%
Safe recovery → process heating
Vacuum residue
0.2–0.5 t2%–5%
Asphalt use, industrial-boiler fuel or compliant handling
10-TONNE EXAMPLE
Typical screening values for project evaluation. Actual recovery and fraction distribution depend on feedstock composition, selected distillation route, fractionation cut points and refining losses. The final closed material balance follows representative testing.
| Stream | Quantity from 10.0 t Feed | Share of Feed | Destination |
|---|---|---|---|
| Regenerated base oil | 8.0–8.5 t | 80%–85% | Fractionation, optional refining and separate grade storage |
| Separated water | <0.5 t | <5% | Separate collection and wastewater treatment |
| Light fraction | ≈0.5 t | ≈5% | Separate collection for fuel use or treatment |
| Non-condensable gas | 0.3–0.5 t | 3%–5% | Recovered as process fuel |
| Vacuum residue | 0.2–0.5 t | 2%–5% | Asphalt use, industrial-boiler fuel or compliant handling |
07
ENGINEERING SOLUTION
Utilities & Energy Consumption
The utility schedule covers electricity, heating, cooling water, instrument air, nitrogen, vacuum duty and the consumables required by the selected distillation and refining routes.
| Utility | Users | Project Output | Main Variables |
|---|---|---|---|
| Electricity | Pumps, vacuum package, fans and PLC | Installed load, running load and kWh/t | Capacity, selected route and automation |
| Heating fuel | Integrated dehydration/light-removal unit and distillation | Fuel type, heating value and hourly use | Feed water, route, heat recovery and load |
| Thermal oil | Thin-film or indirect-heating route | Duty, circulation and supply/return temperature | ≥400°C system rating where >380°C is required |
| Cooling water | Fraction condensers, product coolers and vacuum system | Circulation, makeup and supply/return temperature | Ambient temperature and condensation duty |
| Nitrogen / air | Purging, valves and instruments | Pressure, normal and peak flow | Equipment volume and control-valve count |
| Silica gel / extraction solvent | Selected optional refining route | Consumption, circulation, makeup and recovery | Feedstock and product quality target |
| Hydrogen and hydrotreating utilities | Hydrotreating projects ≥50 T/D only | Hydrogen demand and auxiliary utilities | Feedstock, pressure, catalyst and product target |
DEHYDRATION STAGE
55–180°C
Water removed and collected separately
LIGHT-REMOVAL STAGE
180–260°C
Low-boiling components collected separately
THIN-FILM ROUTE
<20–30 mbar
Typical high-vacuum design target
THERMAL OIL
≥400°C
System rating where high-temperature service is used
ENERGY BASIS
Final electricity, fuel, cooling-water and consumable figures are calculated from feedstock water, the selected batch, continuous or thin-film route, heat recovery, vacuum system, ambient conditions and refining level.
08
ENGINEERING SOLUTION
Major Equipment Configuration
The equipment list identifies each tag, equipment name, process duty, quantity basis and whether the item is standard or optional.
| Section | Tag | Equipment | Duty | Quantity | Scope |
|---|---|---|---|---|---|
| Feedstock | TK-101 | Feedstock receiving/buffer unit | Receiving, homogenization and stable feed | Project-specific | Standard |
| Feedstock | F-101 | Pre-filter | Mechanical impurity removal | Project-specific | Standard |
| Pre-treatment | V-201 | Vacuum dehydration and light-removal unit | Staged water and light-component removal | Project-specific | Standard |
| Route Option | V-401A | Batch twin-kettle vacuum distillation | Alternating batch base-oil recovery | One selected route | Selectable |
| Route Option | H-401B | Continuous tubular-furnace distillation | Continuous base-oil vapour generation | One selected route | Selectable |
| Route Option | WFE-401C | Thin-film distillation system | Short-residence high-vacuum separation | One selected route | Selectable |
| Fractionation | K-501 | Fractionation and reflux system | Separate vapour by boiling range | Project-specific | Standard |
| Fractionation | E-501 | Fraction condensers and receivers | Condense and collect each base-oil fraction | By product cuts | Standard |
| Refining | U-601 | Silica-gel adsorption system | Colour, odour and stability improvement | By product target | Optional |
| Refining | U-602 | Solvent-extraction and recovery system | Selective aromatic and polar-compound removal | By product target | Optional |
| Refining | U-603 | Hydrotreating system | Large-project quality upgrading | Projects ≥50 T/D | Optional |
| Utilities | VP-701 | Roots + dry vacuum package | Maintain <20–30 mbar where required | Project-specific | Standard |
| Utilities | H-801 | Heating system | Tubular furnace or ≥400°C thermal-oil heating | Project-specific | Standard |
| Utilities | FG-802 | NCG safety recovery system | Separation, flame arresting, regulation and fuel reuse | Project-specific | Standard |
| Section | Tag | Equipment | Duty | Quantity | Scope |
|---|---|---|---|---|---|
| Feedstock | TK-101 | Feedstock receiving/buffer unit | Receiving, homogenization and stable feed | Project-specific | Standard |
| Feedstock | F-101 | Pre-filter | Mechanical impurity removal | Project-specific | Standard |
| Section | Tag | Equipment | Duty | Quantity | Scope |
|---|---|---|---|---|---|
| Pre-treatment | V-201 | Vacuum dehydration and light-removal unit | Staged water and light-component removal | Project-specific | Standard |
| Section | Tag | Equipment | Duty | Quantity | Scope |
|---|---|---|---|---|---|
| Route Option | V-401A | Batch twin-kettle vacuum distillation | Alternating batch base-oil recovery | One selected route | Selectable |
| Route Option | H-401B | Continuous tubular-furnace distillation | Continuous base-oil vapour generation | One selected route | Selectable |
| Route Option | WFE-401C | Thin-film distillation system | Short-residence high-vacuum separation | One selected route | Selectable |
| Section | Tag | Equipment | Duty | Quantity | Scope |
|---|---|---|---|---|---|
| Fractionation | K-501 | Fractionation and reflux system | Separate vapour by boiling range | Project-specific | Standard |
| Fractionation | E-501 | Fraction condensers and receivers | Condense and collect each base-oil fraction | By product cuts | Standard |
| Section | Tag | Equipment | Duty | Quantity | Scope |
|---|---|---|---|---|---|
| Refining | U-601 | Silica-gel adsorption system | Colour, odour and stability improvement | By product target | Optional |
| Refining | U-602 | Solvent-extraction and recovery system | Selective aromatic and polar-compound removal | By product target | Optional |
| Refining | U-603 | Hydrotreating system | Large-project quality upgrading | Projects ≥50 T/D | Optional |
| Section | Tag | Equipment | Duty | Quantity | Scope |
|---|---|---|---|---|---|
| Utilities | VP-701 | Roots + dry vacuum package | Maintain <20–30 mbar where required | Project-specific | Standard |
| Utilities | H-801 | Heating system | Tubular furnace or ≥400°C thermal-oil heating | Project-specific | Standard |
| Utilities | FG-802 | NCG safety recovery system | Separation, flame arresting, regulation and fuel reuse | Project-specific | Standard |
Material, design temperature, design pressure, area, motor power and interfaces are defined in individual equipment datasheets.
09
ENGINEERING SOLUTION
Automation & Control System
Choose local PLC + HMI control or a plant-wide PLC + SCADA system. The PLC executes real-time control and interlocks; SCADA adds centralized monitoring, history, alarm management and reporting.
STANDARD CONTROL
PLC + HMI
Local plant operation
ADVANCED CONTROL
PLC + SCADA
Central control room
STANDARD CONTROL
PLC + HMI
Local plant operation with real-time control, alarms, interlocks and operating records.
CONTROL ARCHITECTURE
01
Field Instruments
02
PLC & Remote I/O
03
Local HMI
PLC: real-time control, sequences and interlocks.
HMI: operation, monitoring and records.
ADVANCED CONTROL
PLC + SCADA
Plant-wide supervision with centralized monitoring, historical data, alarm management and production reporting.
CONTROL ARCHITECTURE
01
Field Instruments
02
PLC & Remote I/O
03
Industrial Network
04
SCADA Server
05
Operator / Engineer Stations
PLC: real-time control, sequences and interlocks.
SCADA: operation, monitoring and records.
Temperature
Pressure & Vacuum
Level
Flow
Combustion
Emergency Shutdown
10
ENGINEERING SOLUTION
Safety Interlocks & Off-Gas Treatment
The safety system defines exactly how the plant alarms, isolates heat and feed, and moves to a safe state after high temperature, high pressure, vacuum failure, flame failure or cooling-water loss.
STANDARD NCG SAFETY TRAIN
Entrained liquid is removed before the gas passes through separation, flame arresting, isolation, pressure regulation and buffering. Low pressure, high pressure and flame-failure signals are interlocked with the burner.
| Trigger | Automatic Action | Protection Purpose |
|---|---|---|
| Evaporator / distillation temperature high-high | Alarm, stop feed and cut heating | Prevent overheating and oil degradation |
| System pressure high-high | Cut heat, stop feed and enter safe relief logic | Prevent equipment overpressure |
| Abnormal vacuum | Alarm, limit heat load and inspect condensation/vacuum package | Prevent unstable separation and oxidation |
| Burner flame failure | Close fuel and NCG automatic shut-off valves | Prevent unburned gas from entering the furnace |
| NCG pressure low/high | Isolate NCG fuel and move to safe state | Maintain stable fuel-gas operation |
| Cooling-water failure | Alarm and reduce or stop heat input | Prevent loss of condensation |
| Critical level high-high/low-low | Stop related pump or feed | Prevent overflow and dry running |
| Emergency shutdown | Isolate feed, heat and combustible gas through ESD logic | Bring the plant to a controlled safe state |
11
ENGINEERING SOLUTION
Waste Treatment & Resource Recovery
The plant can combine wastewater treatment, off-gas energy recovery, flue-gas alkali scrubbing and vacuum-residue utilization in one environmental-control system.
01 WASTEWATER
Secondary Discharge
Water condensate from the integrated vacuum unit and oily drainage
VBOLT OPTIONAL SUPPLY Designed to meet the applicable secondary discharge standard after water analysis.
02 OFF-GAS & FLUE GAS
Fuel Recovery + Alkali Scrubbing
NCG is recovered as process fuel; combustion flue gas is cleaned before discharge.
ENERGY RECOVERY Demisting, separation, flame arresting and pressure control protect the fuel-gas route.
03 VACUUM RESIDUE
Resource Utilization
Vacuum residue is collected separately from filter solids and refining by-products.
ASPHALT PLANT
Raw material for asphalt blending or road paving
BOILER FUEL
Industrial energy recovery when properties and local rules permit
SEPARATE HANDLING Filter solids, spent silica gel, extraction by-products and hydrotreating catalyst are handled by qualified contractors as applicable.
Final wastewater and air-emission limits, residue classification and utilization routes follow the project location’s regulations and representative laboratory analysis.
12
ENGINEERING SOLUTION
Plant Layout & Installation Conditions
The layout follows process flow, vacuum equipment elevation, safety spacing, operating access, lifting and maintenance routes, utility tie-ins and future expansion requirements.
01 Feedstock & Pre-treatment
02 Integrated Dehydration & Light Removal
03Selected Distillation Route
04 Fractionation & Fraction Condensation
05 Optional Refining & Utilities
06 Client Tank Farm & Loading
Required Client Site Conditions
Site dimensions and soil data · transport and lifting access · foundations · power and grounding · cooling-water tie-ins · fuel or thermal-oil interfaces · instrument air · fire protection · separate product-grade tanks
13
ENGINEERING SOLUTION
What VBOLT Supplies
VBOLT supplies the engineered base-oil recovery plant, in-skid systems, selected automation and project services up to clearly marked connection points.
VBOLT SUPPLY
Inside the process-plant boundary
Engineering, vacuum process equipment, auxiliaries, automation and project services are supplied to the defined battery limits.
01
Engineering & Documents
Process design, layout, datasheets, control logic and interface documents
02
Main Process Equipment
Pre-treatment, integrated dehydration and light removal, one selected distillation route, fractionation and fraction condensation
03
Auxiliary Systems
High vacuum, heating, condensation, NCG recovery and grade-separated transfer
04
Automation & Safety
PLC/HMI or PLC/SCADA, instruments, alarms and safety interlocks
05
In-Skid Piping
Piping, valves, supports and connections inside the equipment boundary
06
Commissioning & Training
Installation guidance, trial operation, acceptance support and operator training
CLIENT CONSTRUCTION
What the Client Needs to Build
The client constructs the foundations, grade-separated tank farm, loading area, external utilities, fire-protection system and site connections shown in blue.
01
Civil Works & Foundations
Site grading, equipment foundations, plant building, roads and drainage
02
Plant Building & Steelwork
Operating platforms, stairs and site structural steel outside VBOLT skids
03
Feedstock & Product Tank Farm
Waste-oil tanks, separate base-oil grade tanks, light-fraction tanks and tank-farm piping
04
Loading & Unloading Area
Truck unloading, product loading, transfer pumps and site piping
05
External Utilities
Power, fuel, cooling water, instrument air, nitrogen and drainage connections
06
Fire Protection & Site Safety
Fire water, extinguishing systems, alarms, grounding and emergency access
15
ENGINEERING SOLUTION
Installation, Commissioning & Acceptance
Four controlled stages define the work, deliverables, client support and release gate from approved design to final plant handover.
TURNKEY DELIVERY CONTROL
From Design Freeze to Plant Handover
STAGE 01
Engineering
Confirm feedstock, capacity, product target, utilities and site interfaces.
DELIVERABLE
Approved process, layout, equipment and control documents
CLIENT SUPPORT
Provide project inputs and approve interface documents
RELEASE GATE
Drawings approved
STAGE 02
Manufacturing & Delivery
Fabricate, inspect, pressure-test, preserve, mark, pack and ship the equipment.
DELIVERABLE
Equipment, inspection dossier and packing list
CLIENT SUPPORT
Complete the site and prepare lifting and receiving resources
RELEASE GATE
Ready for shipment
STAGE 03
Installation & Start-up
Verify installation, complete cold testing, hot circulation and gradual feed-in.
DELIVERABLE
Installation checks, test records and commissioning report
CLIENT SUPPORT
Provide utilities, qualified feedstock and operating personnel
RELEASE GATE
Stable operation
STAGE 04
Acceptance & Handover
Run under agreed conditions, sample the product and complete operator training.
DELIVERABLE
Performance record, test results and operating documents
CLIENT SUPPORT
Participate in sampling, testing and final sign-off
RELEASE GATE
Acceptance signed
16
ENGINEERING SOLUTION
Operators & Maintenance
Staffing and maintenance are defined by plant capacity, batch or continuous operating mode, automation level, refining route and the client’s existing maintenance and laboratory resources.
Operating Roles
| Role | Main Duty | Basis |
|---|---|---|
| Shift Supervisor | Start-up, shutdown, adjustment and handover | Per shift |
| Field Operator | Inspection, sampling, drains, filtration and transfer | By plant size |
| Electrical / Instrument | PLC, instruments, motors and interlocks | Shared or dedicated |
| Mechanical / Vacuum | Pumps, seals, evaporator, exchangers and vacuum package | Shared or dedicated |
| Laboratory | Feed, intermediate cuts and finished base-oil testing | By laboratory plan |
Maintenance Frequency
| Frequency | Main Work |
|---|---|
| Each Shift | Temperature, vacuum, level, pumps, leaks, product cuts and alarms |
| Weekly | Filter differential pressure, condensate drains, vacuum seals and standby equipment |
| Monthly | Valve stroke, interlock test, instrument comparison and electrical tightening |
| Quarterly | Evaporator surfaces, condensers, vacuum system, heating and safety accessories |
| Annual | Planned shutdown, internal cleaning, calibration and interlock validation |
17
ENGINEERING SOLUTION
Project References & Third-Party Testing
A credible base-oil project reference connects site photographs to feedstock, capacity, distillation route, operating record, viscosity cuts and the corresponding product test report.
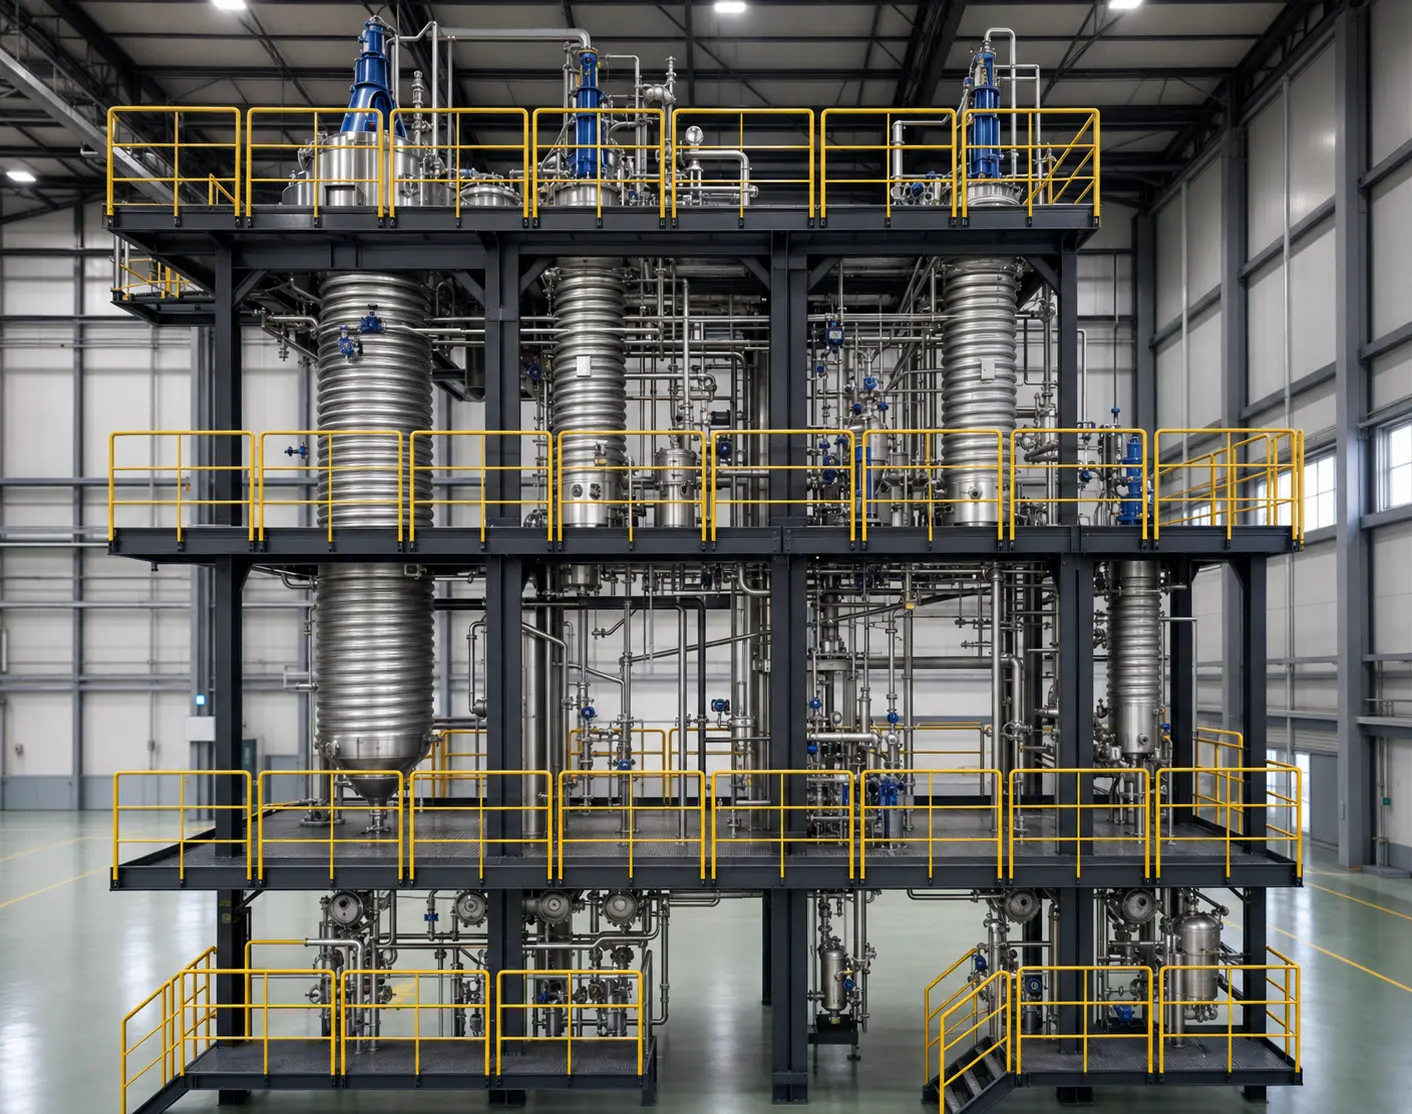
Third-Party Verification
Every published result should identify the sample source, viscosity grade, sampling date, test methods, report number and associated production batch.
18
ENGINEERING SOLUTION
Client Project Data Form
Submit feedstock, capacity, operating mode, target base-oil grades, refining level, utilities and site data so VBOLT can define the process route, equipment sizes, consumption and battery limits.
PROJECT INPUT
Engineering starts with real project data.
Better feedstock and viscosity data produces a more reliable material balance, route selection, equipment list, energy estimate and product assessment.
01 Feedstock & Capacity
02 Base Oil & Refining
03Utilities & Site
04 Contact & Requirements